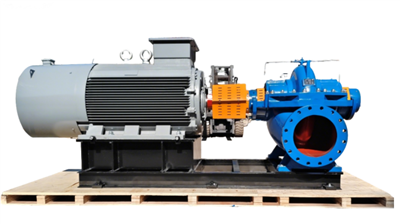
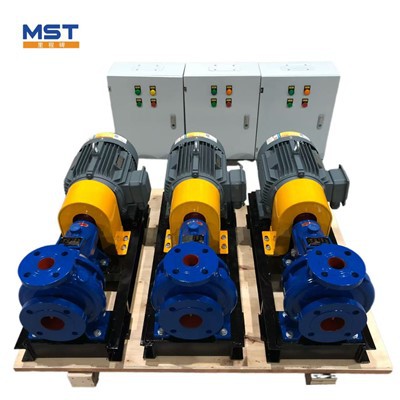
High flow split case pumps In modern industrial equipment, pump performance directly impacts production efficiency and system stability. High flow split case pumps, as highly efficient and energy-saving fluid transfer devices, have become the preferred choice for many...
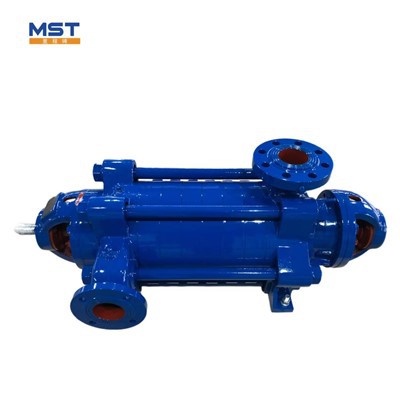
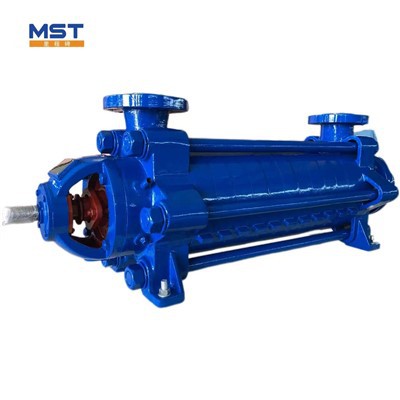
As a high head Multi impeller Pump, the High head Multi impeller pump has seen rapid adoption in both industrial and civil applications in recent years due to its excellent performance and wide range of uses. With its unique design concept and superior operational...
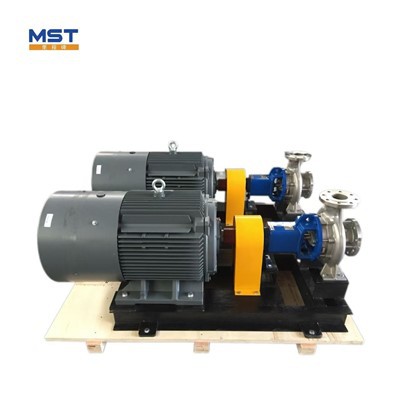
When it comes to transferring 100°C hot water in industrial plants, commercial buildings, or heating systems, the 100°C Hot Water 30KW Pump stands out as a robust and efficient solution designed to meet the most demanding thermal transfer requirements. Engineered with...
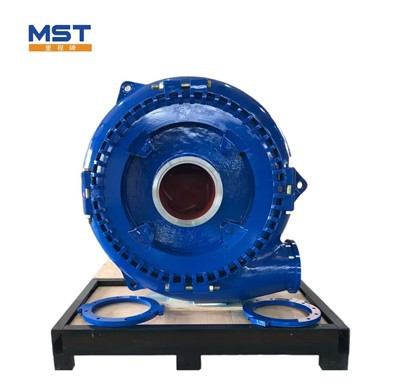
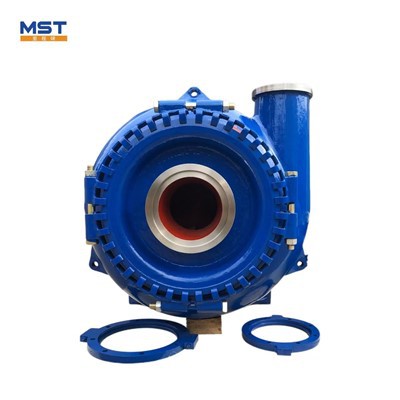
The large-channel gravel pump is a high-efficiency pump specifically designed for conveying media containing large particles of gravel, slurry, and slag. It features 18-inch inlet (inlet) and 16-inch outlet (outlet) diameters, meeting the demands of high flow rates and high...
The 110℃ 350m Boiler Feed Water Pump stands as a reliable and efficient core component for industrial boiler systems, specifically engineered to meet the demanding requirements of transferring feedwater at a maximum temperature of 110℃ and a head of 350 meters. Designed for...
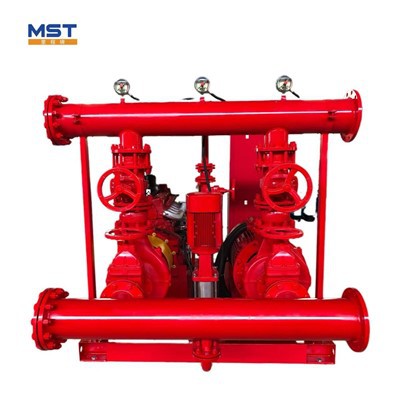
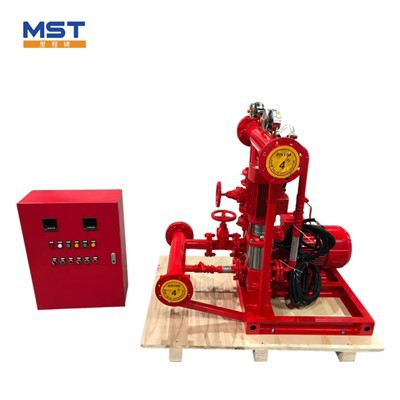
In high-stakes environments where fire safety can mean the difference between minor incidents and catastrophic losses, our 150GPM 11Bar 37kw Fire Pump stands as a trusted, high-performance solution engineered to meet the most demanding fire suppression needs. Designed in...
Water conservancy project pumps are indispensable equipment in modern water conservancy facilities, undertaking the key tasks of water transportation, irrigation and drainage, and various water conservancy project operations. This article introduces a high-quality hydraulic...
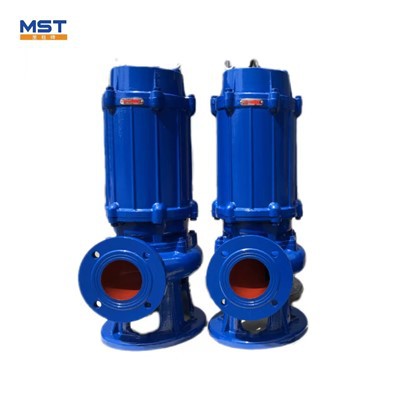
In the field of municipal wastewater management, efficient and reliable pumping equipment is crucial for ensuring smooth sewage transportation and treatment processes. The 45 l/s Submersible Pump for Wastewater Municipal stands out as a high-performance solution tailored to...
Vertical fire pumps are crucial equipment in fire protection systems, rapidly providing strong and stable water pressure during a fire to ensure the normal operation of firefighting equipment and protect personnel and property. This article will introduce the basic concepts,...
When it comes to efficient, reliable handling of abrasive and high-density slurry in mining, construction, or industrial wastewater treatment, the SG1.6 250m³ 80m Slurry Pump stands out as a high-performance solution tailored to meet heavy-duty operational demands....
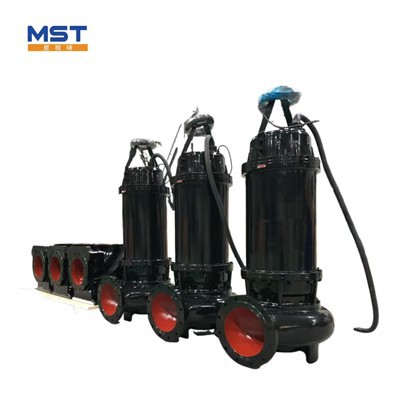
The 300WQ1000-25-110 large-channel submersible sewage pump is a high-performance, advanced-structure, and highly efficient conveying device, particularly suitable for various sewage treatment and discharge projects. This model features a large 300mm diameter outlet and a...
Boiler feedwater pumps are key equipment in boiler systems, primarily responsible for delivering feedwater into the boiler for heating to generate steam. Boiler feedwater pumps typically feature multiple impellers, high temperature resistance, high pressure, and high head.